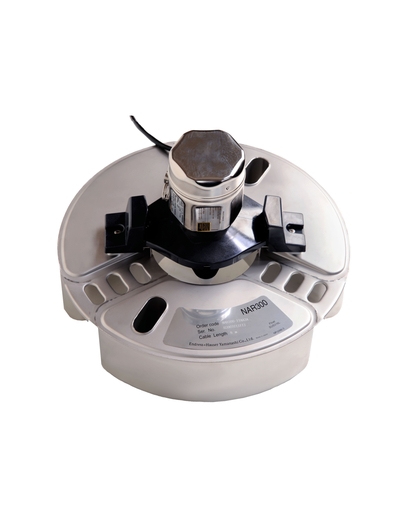
Installed in the drainage pit near the tank or pump, the NAR300 system provides outstanding leak detection for oil, vegetable oil and more. The tuning fork and electronic vibration technology combined with two-position logic provide simple, safe and highly reliable outputs for leak monitoring.
Benefits
-
Two independent sensors used together for precise liquid leak detection
-
Conductive probe detects water or non-aqueous liquids
-
Electronic vibration tuning fork confirms oil or air
-
No moving parts, long service life and reduced maintenance costs
-
Alarm output in the event of cable failure or water freezing, fail-safe
-
Measures non-water-soluble liquids, independent of dielectric constant
Applications
Ambient temperature: -20...+60°C (-4...+140°F)
Source: Endress+Hauserpublic information from the website
Spare Parts & Accessories 6
6 spare parts · click to collapse
| Order code | Description | |
|---|---|---|
| 56004365 | Floating roof sensor cover plate, plasticUsage: NAR300. | Details |
| 71137732 | Operating and Adjustment ToolUsage: NAR300. | Details |
| 56004438 | I/F Ex junction box internal mounting plate, TIISUsage: NAR300. | Details |
| 71276647 | NAR300 Sensor I/F assy, FM/ATEX/IECEx/JPN | Details |
| 56004306 | NRR261/Ex Junction Box CoverSmall terminal box cover, AC, E+H gray. Usage: NRR261/Ex Interface Box. | Details |
| 017880-5026 | O-ring, terminal box, small, CRSize: D100mm, d3mm. Material: CR (Chloroprene Rubber). Part: terminal box, small. Usage: AT1/AT500, DRM9700, DU, NRR261/NRR263, NMT539 Converter, TGM5. | Details |
Configurator / Comparison
Manuals & Documents 12
All documents for this model12 documents · click to expand
BA NAR300系统 Chinese
BA 适用高温工况的NAR300系统 Chinese
BA NAR300 system English
BA NAR300 system for high temperature English
NAR300 system - Operating Instruction English
NAR300 system - Operating Instruction English
BA NAR300 system English
BA NAR300 system for high temperature English
TI 油泄漏检测器NAR300 Chinese
TI 油泄漏检测器NAR300,适用高温工况 Chinese
TI Oil leak detector NAR300 English
TI Oil leak detector NAR300 for high temperature English
Case Studies
Municipal Wastewater Treatment · tank farm — Application Case
Application Context
the inlet, biological and outlet stages of a municipal plant is a typical Municipal Wastewater Treatment duty. The project started from tank farm, focusing on centralised level and inventory gauging across a tank farm.
Process Constraints
effluent parameters drift and probes foul with sludge and biofilm, and high solids and corrosive fractions, with large diurnal flow swings only amplify it. The tank farm specification must therefore cover choosing the gauging method by tank size, medium and safety class, then networking them together.
Delivery Approach
Delivery was handled as the level range — level solution matched to the actual tank and silo geometry. Execution centred on choosing the gauging method by tank size, medium and safety class, then networking them together, together with stable compliance with Grade 1A discharge limits and online data reporting.
Field Results
Operation shows the benefit clearly — real-time inventory, making stocktaking and loss accounting more accurate, with confidence in this measuring point improving markedly.
Food & Beverage · tank farm — Application Case
Customer Profile
The typical setting in Food & Beverage is dosing, pasteurising, filling and CIP stages. The measuring point is tank farm; the focus is centralised level and inventory gauging across a tank farm.
Key Difficulties
Conditions are syrups, dairy and beverages that scale easily, under strict hygienic requirements and, on top of that, frequent cleaning demands instruments that withstand hot CIP/SIP caustic cycles, which a standard configuration cannot handle for long. The design therefore starts with choosing the gauging method by tank size, medium and safety class, then networking them together.
Implementation
The scope ran through the level range: level solution matched to the actual tank and silo geometry. Technically it hinges on choosing the gauging method by tank size, medium and safety class, then networking them together, and on these requirements: food-safety and hygienic design per 3-A / EHEDG.
Customer Benefit
In practice this means real-time inventory, making stocktaking and loss accounting more accurate, which cut the workload on the site maintenance team.
Chemical & Pharmaceutical · tank farm — Application Case
Project Background
The project covers reactors, metering vessels and finished-product tanks. The work centres on tank farm and the core task is centralised level and inventory gauging across a tank farm.
Operating Challenges
The medium and duty are characterised by highly corrosive media with solvents and crystallisation, partly in explosive atmospheres, and corrosion plus Ex protection shortens instrument life and makes downtime costly. So tank farm cannot be specified generically — it calls for choosing the gauging method by tank size, medium and safety class, then networking them together.
Solution
The Ainstru engineering team worked through the level range: level solution matched to the actual tank and silo geometry. The configuration involves choosing the gauging method by tank size, medium and safety class, then networking them together, with these requirements in view: Ex certification and GMP traceability of records.
Results
Since start-up the system has run steadily; the practical result is real-time inventory, making stocktaking and loss accounting more accurate.
Power & Energy · tank farm — Application Case
Project Overview
The site is boiler feedwater, turbine condensate and FGD/DeNOx systems. The customer wanted tank farm properly configured on the existing plant, with the aim of centralised level and inventory gauging across a tank farm.
Technical Challenges
What actually causes trouble is high temperature and pressure with both steam and saline water, and drift under high temperature and pressure, with very costly unplanned outages. All of this means the tank farm configuration has to involve choosing the gauging method by tank size, medium and safety class, then networking them together.
Configuration
Supply and installation were organised through the level range: level solution matched to the actual tank and silo geometry. On site this meant choosing the gauging method by tank size, medium and safety class, then networking them together, checked line by line against: compliance with power-industry codes and unit availability targets.
Performance
After commissioning the outcome is real-time inventory, making stocktaking and loss accounting more accurate, and the readings are now used for process tuning.
Related Products
 Endress+Hauser
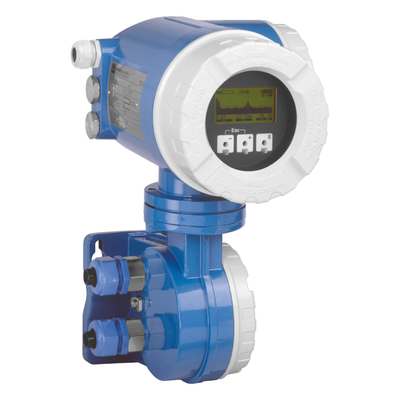
Tank Side Monitor NRF590
 Endress+Hauser
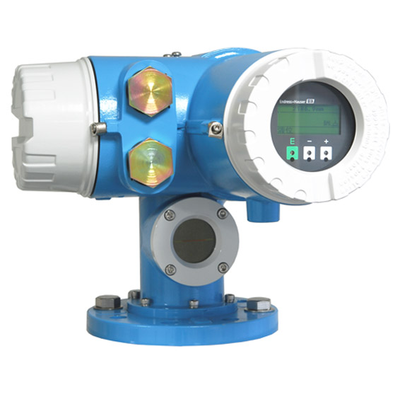
Proservo NMS5
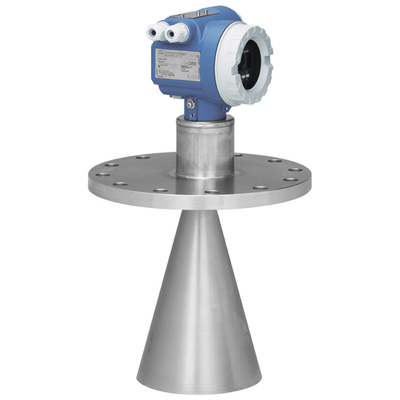 Endress+Hauser
Micropilot S FMR530
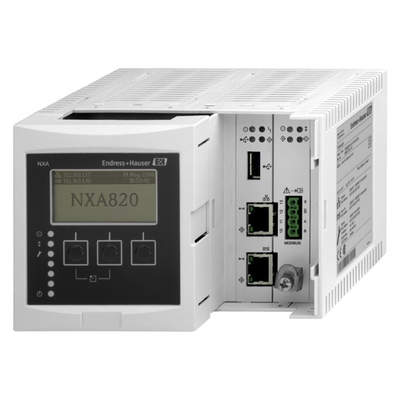 Endress+Hauser
Tankvision Tank Scanner NXA820
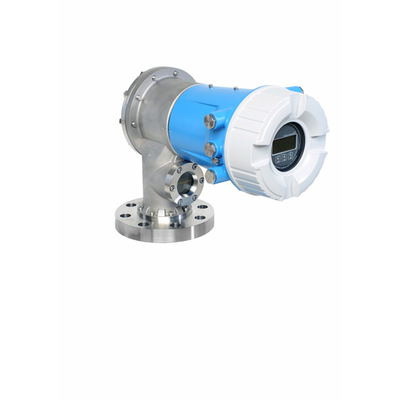 Endress+Hauser
Servo tank gauge NMS81
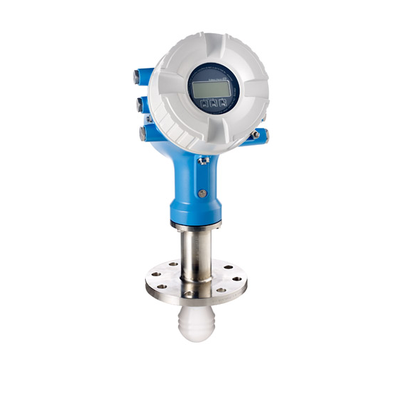 Endress+Hauser
Radar level transmitter NMR81
 Endress+Hauser
Float level transmitter
 Endress+Hauser