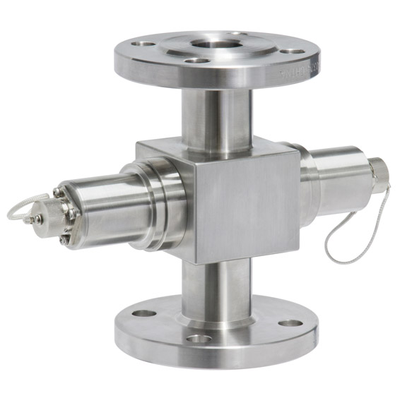
Sensor OUSAF12
Technical Data
CompareConcentration
| Measuring Principle | Colorimetry |
| Application | Color measurement, measurement of suspendend solids, phase separation |
| Measuring range | 0 to 2.5 AU 0 to 50 OD (depending on optical pathlength) |
| Material | Sensor housing: Stainless Steel 316L |
| Process temperature | 0 to 90 °C (32 to 194 °F) continuous Max. 130 °C (266 °F) for 2 hours |
| Process pressure | Max. 100 bar abs (1450 psi) (depending on flow through assembly) |
| Ex certification | ATEX II 2G Ex db IIC T5 Gb FM Cl.1, Div. 1, Group B, C, D |
| Ingress protection | IP 65 (NEMA 4) |
| Certificates, declarations and approvals | FDA |
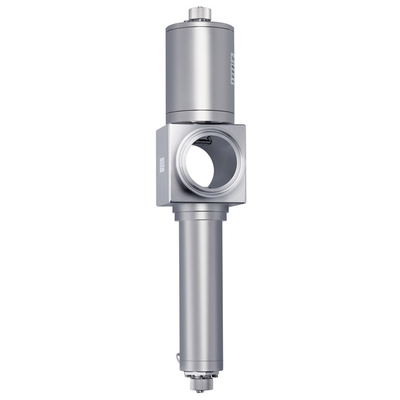
The OUSAF12 is an optical sensor for the online detection of suspended solids concentration and product interfaces in many industries. Through absorbance measurement, it effectively helps you precisely control product quality and process, thereby improving production efficiency. The OUSAF12 sensor can measure in explosion-proof areas and hygienic (CIP/SIP) process applications.
Advantages
Better product quality monitoring in pharmaceutical and chemical processes
Fast interface detection saves costs and reduces product loss
Low sensor maintenance, long service life and stable operation
Color independent of measurement
Simple liquid-free verification
Resistant to CIP and SIP cleaning
Explosion protection approval for use in explosive hazardous areas
Areas of application
The OUSAF12 turbidity or color sensor can be used for:
Quality control / purity monitoring
Filtration monitoring
Condensate monitoring
Brewery turbidity
Heat exchanger leak monitoring
Brine turbidity
International explosion protection approvals such as ATEX and FM; the sensor can be used in explosive hazardous areas
E+H Product Configurator
Please enter the product order code to configure
Product comparison
Please enter the order codes of the products to compare in the boxes below (up to three products)
Technical documentation
Technical data
Documents/Manuals/Software
Accessories/Spare parts
Source:Endress+Hauserwebsite public information
Case Studies
Municipal Wastewater Treatment — Wastewater Treatment Plant · Turbidity Application Case
Project Background
Municipal Wastewater Treatment customers at the Wastewater Treatment Plant stage have long faced the challenge of insufficient accuracy in effluent quality monitoring and instruments prone to contamination causing data drift, affecting compliance discharge, placing higher demands on the stability and measurement accuracy of Turbidity.
Solution
Based on the on-site conditions, the Ainstru technical team selected suitable Turbidity for the customer and delivered one-stop service covering selection, installation, commissioning and tuning.
Results
- Measurement accuracy and response speed significantly improved, with stable and reliable data;
- Instruments adapt to complex Municipal Wastewater Treatment conditions, greatly reducing maintenance;
- Helping customers achieve continuous online monitoring and cost reduction, highly recognized by customers.
Food & Beverage — Food Production Line · Turbidity Application Case
Project Background
Food & Beverage customers at the Food Production Line stage have long faced the challenge of high hygienic measurement requirements, with inline instruments needing to withstand CIP/SIP cleaning while maintaining stable accuracy, placing higher demands on the stability and measurement accuracy of Turbidity.
Solution
Based on the on-site conditions, the Ainstru technical team selected suitable Turbidity for the customer and delivered one-stop service covering selection, installation, commissioning and tuning.
Results
- Measurement accuracy and response speed significantly improved, with stable and reliable data;
- Instruments adapt to complex Food & Beverage conditions, greatly reducing maintenance;
- Helping customers achieve continuous online monitoring and cost reduction, highly recognized by customers.
Chemical & Pharmaceutical — Reactors and Storage Tanks · Turbidity Application Case
Project Background
Chemical & Pharmaceutical customers at the Reactors and Storage Tanks stage have long faced the challenge of highly corrosive media and complex conditions, requiring corrosion-resistant and explosion-proof instruments, placing higher demands on the stability and measurement accuracy of Turbidity.
Solution
Based on the on-site conditions, the Ainstru technical team selected suitable Turbidity for the customer and delivered one-stop service covering selection, installation, commissioning and tuning.
Results
- Measurement accuracy and response speed significantly improved, with stable and reliable data;
- Instruments adapt to complex Chemical & Pharmaceutical conditions, greatly reducing maintenance;
- Helping customers achieve continuous online monitoring and cost reduction, highly recognized by customers.
Power & Energy — Power Plant Boiler and Turbine · Turbidity Application Case
Project Background
Power & Energy customers at the Power Plant Boiler and Turbine stage have long faced the challenge of unstable measurement under high temperature and pressure, with high maintenance and downtime costs, placing higher demands on the stability and measurement accuracy of Turbidity.
Solution
Based on the on-site conditions, the Ainstru technical team selected suitable Turbidity for the customer and delivered one-stop service covering selection, installation, commissioning and tuning.
Results
- Measurement accuracy and response speed significantly improved, with stable and reliable data;
- Instruments adapt to complex Power & Energy conditions, greatly reducing maintenance;
- Helping customers achieve continuous online monitoring and cost reduction, highly recognized by customers.
Related Products
 Endress+Hauser
Turbimax CUS52D
 Endress+Hauser
Turbimax CUS51D
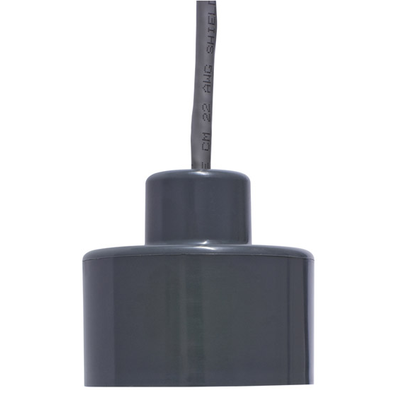 Endress+Hauser
Turbimax CUS71D
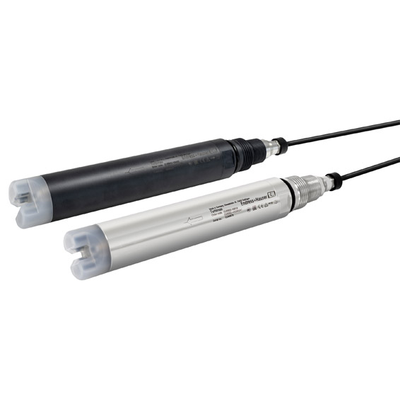 Endress+Hauser
Turbimax CUS50D
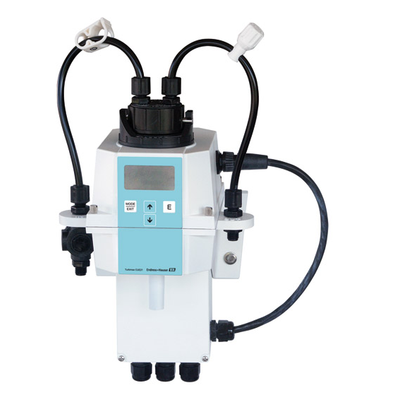 Endress+Hauser
Turbimax CUE22, compact white light
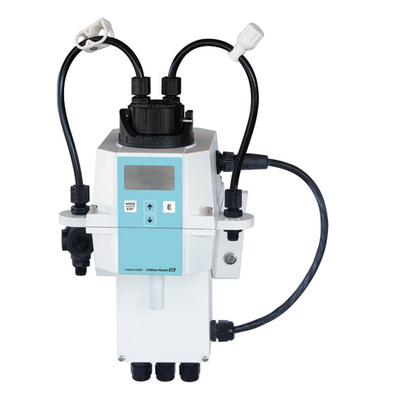 Endress+Hauser
Turbimax CUE21, compact infrared
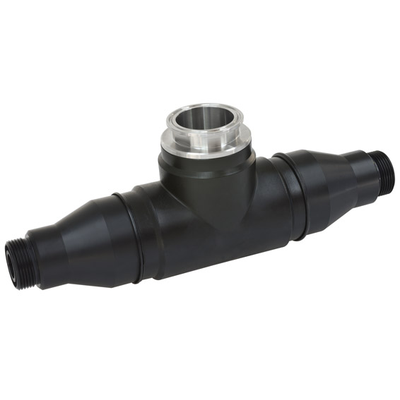 Endress+Hauser
Flowfit CUA252
 Endress+Hauser