Technical Data
CompareConcentration
| Measuring Principle | NIR absorbance |
| Application | Turbidity and suspended solids measurement for filter control and quality measurement |
| Measuring range | 0 to 200 FTU 0 to 200 ppm DE |
| Material | Sensor housing: 316L |
| Process temperature | 0 to 90 °C (32 to 194 °F) continuous Max. 130 °C (266 °F) for 2 hours |
| Process pressure | Max. 100 bar (1450 psi) (depending on flow through assembly) |
| Ex certification | ATEX II 2G Ex db IIC T5 Gb FM Cl.1, Div. 1, Group B, C, D |
| Ingress protection | IP 65 (NEMA 4) |
| Certificates, declarations and approvals | FDA |
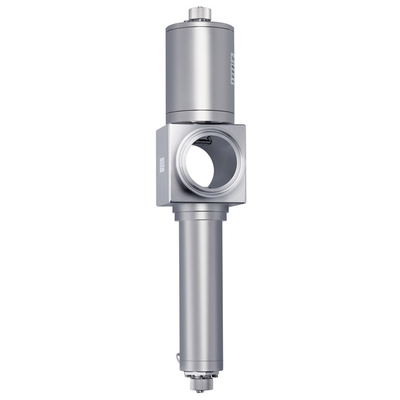
The OUSTF10 scattered light turbidity sensor is used to measure suspended solids, emulsions and immiscible fluids in process liquids. It provides you with all the information you need, from product purity to filter blockage. This allows you to better control your products and processes. The OUSTF10 works in a wide range of environments, such as: extremely high temperatures, hazardous areas (ATEX, FM) and hygienic processes (CIP/SIP).
Benefits
Precise, highly sensitive purity monitoring for better product quality
Low maintenance, long service life and stable operation
Optional long-range near-infrared (NIR) filter reduces measurement errors caused by color
Reliable leak detection in heat exchangers
Resistant to SIP / CIP cleaning
Explosion-protection approval for use in hazardous areas
Applications
The OUSTF10 sensor is used for turbidity measurement:
Quality control / purity monitoring
Filter monitoring
Condensate monitoring
Turbidity measurement in breweries
Heat exchanger leak detection
Saltwater turbidity
International explosion-protection approvals, such as ATEX and FM, for use in hazardous areas
Spare Parts & Accessories 2
Configurator / Comparison
Source: Endress+Hauserpublic information from the website
Measuring principle video
 Click to play
Manuals & Documents 5
All documents for this modelCase Studies
Municipal Wastewater Treatment · turbidity — Application Case
Project Background
The project covers the inlet, biological and outlet stages of a municipal plant. The work centres on turbidity and the core task is measuring turbidity as an indicator of suspended solids and filtration.
Operating Challenges
The medium and duty are characterised by high solids and corrosive fractions, with large diurnal flow swings, and effluent parameters drift and probes foul with sludge and biofilm. So turbidity cannot be specified generically — it calls for choosing 90° scatter or surface scatter by range, with de-bubbling.
Solution
The Ainstru engineering team worked through the analyser range: selecting as part of a complete water-analysis system. The configuration involves choosing 90° scatter or surface scatter by range, with de-bubbling, with these requirements in view: stable compliance with Grade 1A discharge limits and online data reporting.
Results
Since start-up the system has run steadily; the practical result is backwashing triggered by water quality, saving water while holding quality.
Food & Beverage · turbidity — Application Case
Project Overview
The site is dosing, pasteurising, filling and CIP stages. The customer wanted turbidity properly configured on the existing plant, with the aim of measuring turbidity as an indicator of suspended solids and filtration.
Technical Challenges
What actually causes trouble is syrups, dairy and beverages that scale easily, under strict hygienic requirements, and frequent cleaning demands instruments that withstand hot CIP/SIP caustic cycles. All of this means the turbidity configuration has to involve choosing 90° scatter or surface scatter by range, with de-bubbling.
Configuration
Supply and installation were organised through the analyser range: selecting as part of a complete water-analysis system. On site this meant choosing 90° scatter or surface scatter by range, with de-bubbling, checked line by line against: food-safety and hygienic design per 3-A / EHEDG.
Performance
After commissioning the outcome is backwashing triggered by water quality, saving water while holding quality, and the readings are now used for process tuning.
Chemical & Pharmaceutical · turbidity — Application Case
Site Conditions
This is a Chemical & Pharmaceutical customer whose plant is at reactors, metering vessels and finished-product tanks. The main task was measuring turbidity as an indicator of suspended solids and filtration.
The Problem
The difficulty lies in highly corrosive media with solvents and crystallisation, partly in explosive atmospheres; at the same time corrosion plus Ex protection shortens instrument life and makes downtime costly. Specification therefore means choosing 90° scatter or surface scatter by range, with de-bubbling.
What We Did
We took a analyser range approach — selecting as part of a complete water-analysis system. Delivery was built around choosing 90° scatter or surface scatter by range, with de-bubbling, with point-by-point checks on: Ex certification and GMP traceability of records.
Operating Outcome
In service the system performs as intended — backwashing triggered by water quality, saving water while holding quality, with routine maintenance falling noticeably.
Power & Energy · turbidity — Application Case
Application Context
boiler feedwater, turbine condensate and FGD/DeNOx systems is a typical Power & Energy duty. The project started from turbidity, focusing on measuring turbidity as an indicator of suspended solids and filtration.
Process Constraints
drift under high temperature and pressure, with very costly unplanned outages, and high temperature and pressure with both steam and saline water only amplify it. The turbidity specification must therefore cover choosing 90° scatter or surface scatter by range, with de-bubbling.
Delivery Approach
Delivery was handled as the analyser range — selecting as part of a complete water-analysis system. Execution centred on choosing 90° scatter or surface scatter by range, with de-bubbling, together with compliance with power-industry codes and unit availability targets.
Field Results
Operation shows the benefit clearly — backwashing triggered by water quality, saving water while holding quality, with confidence in this measuring point improving markedly.
Related Products
 Endress+Hauser
Turbimax CUS52D
 Endress+Hauser
Turbimax CUS51D
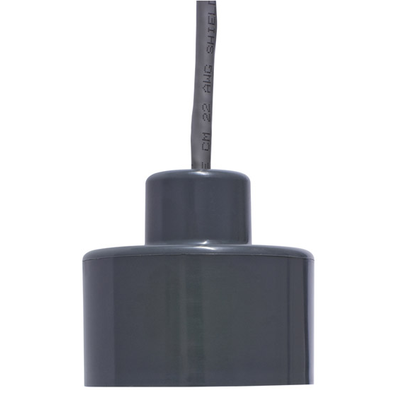 Endress+Hauser
Turbimax CUS71D
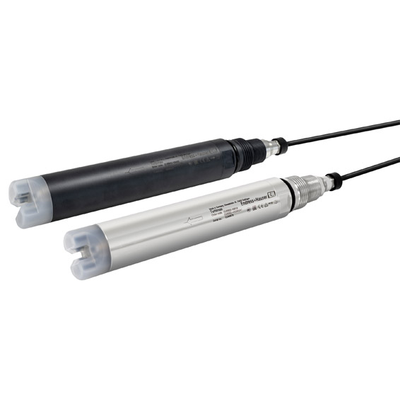 Endress+Hauser
Turbimax CUS50D
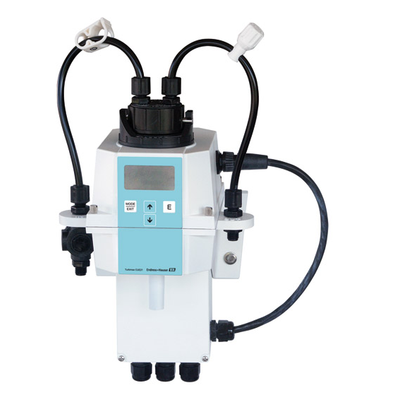 Endress+Hauser
Turbimax CUE22, compact white light
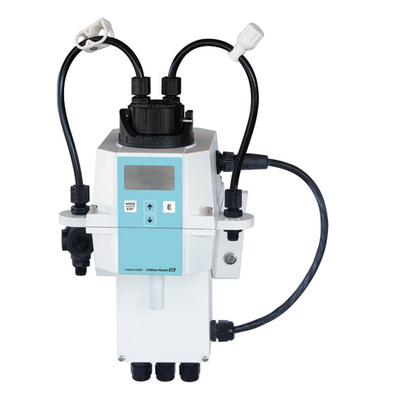 Endress+Hauser
Turbimax CUE21, compact infrared
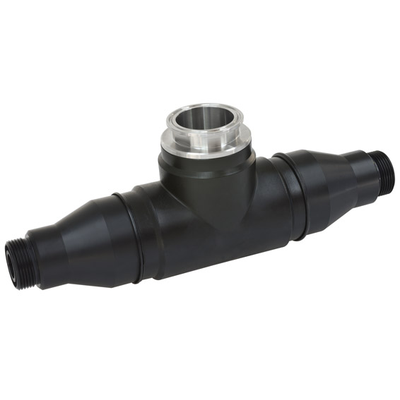 Endress+Hauser
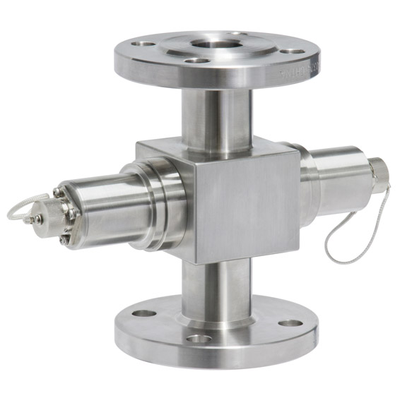
Flowfit CUA252
 Endress+Hauser