Technical Data
CompareSoftware
| Measuring Principle | Inventory Management Solutions |
| Application Task | Data acquisition Data management Process monitoring & visualization |
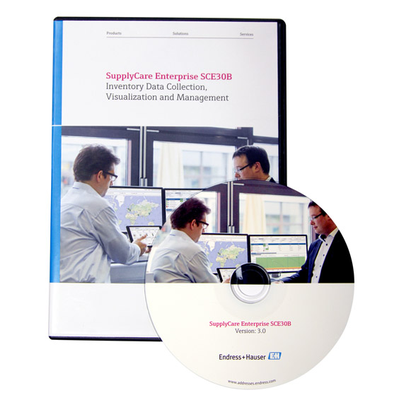
| Field of Application | SupplyCare Enterprise SCE30B is a web-based operating program for the indication and monitoring of levels of e.g. tanks, silos and container spread all over the world. |
| Operating systems | Windows 10 ® (Enterprise) Windows 11 ® (Enterprise) Windows Server 2016 (Standard) Windows Server 2019 (Standard) Windows Server 2022 (Standard) |
| Processor type | 4 cores, 3 GHz or better |
| Main memory | 8 GB (free memory) |
| Hard-disk capacity | 50 GB for full installation, depending on database size |
| Monitor resolution, display | 1280 x 800 (Desktop), application can also be used on mobile devices |
| Interfaces | Web Browser |
| Other | SupplyCare Enterprise runs by default in an Apache Tomcat-environment on an application server as service under Microsoft Windows. The operators and administrators operate the application via web browser from theirs desks. Graphics: The minimum requirements do not take into account the requirements for the server operating system or other applications (e.g. antivirus software) installed on the server. The actual requirements and product functions can depend on the system configuration and the operating system. The requirements for the hardware will depend greatly on the desired number of users, failsafe performance etc.. |
The SupplyCare inventory management platform supports users in developing collaborative demand planning, event-driven replenishment planning and scheduling, as well as reconciliation of geographically distributed inventory (inbound/outbound) and stock taking (total). You can invite partners from all entities, even partners from other companies, making your supply chain more intelligent. The enterprise version can be installed directly on your server.
Advantages
-
Improved demand planning and reduced inventory
-
Initiates business processes such as vendor managed inventory and supplier managed inventory (VMI, SMI)
-
Complete solution from inventory management and data acquisition to business process integration
-
Global service and support network
-
Faster response to supply chain changes
-
View complete inventory anytime, anywhere within the enterprise, even on mobile devices
Application
-
Monitor product inventory in tanks and silos on desktop or via web browser technology
-
Assign warning and alarm limits to all monitored inventory data
-
Send or receive e-mail notifications, e.g. when replenishment is needed
-
Output inventory data in universal or standard formats
-
View trends, historical data and events
-
Manage tanks, tank groups, customers and products
-
Set different viewing permissions for suppliers, third parties and internal users
Accessories/Spare parts
Source:Endress+Hauserwebsite public information
Configurator / Comparison
Manuals & Documents 7
All documents for this model7 documents · click to expand
Case Studies
Municipal Wastewater Treatment · data manager — Application Case
Site Conditions
This is a Municipal Wastewater Treatment customer whose plant is at the inlet, biological and outlet stages of a municipal plant. The main task was centralised data acquisition, storage and forwarding to management platforms.
The Problem
The difficulty lies in high solids and corrosive fractions, with large diurnal flow swings; at the same time effluent parameters drift and probes foul with sludge and biofilm. Specification therefore means selected by channel count, storage depth and forwarding protocol.
What We Did
We took a system components range approach — supplying as a full cabinet and signal-chain configuration. Delivery was built around selected by channel count, storage depth and forwarding protocol, with point-by-point checks on: stable compliance with Grade 1A discharge limits and online data reporting.
Operating Outcome
In service the system performs as intended — automatic backfill after outages, greatly improving data completeness, with routine maintenance falling noticeably.
Food & Beverage · data manager — Application Case
Application Context
dosing, pasteurising, filling and CIP stages is a typical Food & Beverage duty. The project started from data manager, focusing on centralised data acquisition, storage and forwarding to management platforms.
Process Constraints
frequent cleaning demands instruments that withstand hot CIP/SIP caustic cycles, and syrups, dairy and beverages that scale easily, under strict hygienic requirements only amplify it. The data manager specification must therefore cover selected by channel count, storage depth and forwarding protocol.
Delivery Approach
Delivery was handled as the system components range — supplying as a full cabinet and signal-chain configuration. Execution centred on selected by channel count, storage depth and forwarding protocol, together with food-safety and hygienic design per 3-A / EHEDG.
Field Results
Operation shows the benefit clearly — automatic backfill after outages, greatly improving data completeness, with confidence in this measuring point improving markedly.
Chemical & Pharmaceutical · data manager — Application Case
Customer Profile
The typical setting in Chemical & Pharmaceutical is reactors, metering vessels and finished-product tanks. The measuring point is data manager; the focus is centralised data acquisition, storage and forwarding to management platforms.
Key Difficulties
Conditions are highly corrosive media with solvents and crystallisation, partly in explosive atmospheres and, on top of that, corrosion plus Ex protection shortens instrument life and makes downtime costly, which a standard configuration cannot handle for long. The design therefore starts with selected by channel count, storage depth and forwarding protocol.
Implementation
The scope ran through the system components range: supplying as a full cabinet and signal-chain configuration. Technically it hinges on selected by channel count, storage depth and forwarding protocol, and on these requirements: Ex certification and GMP traceability of records.
Customer Benefit
In practice this means automatic backfill after outages, greatly improving data completeness, which cut the workload on the site maintenance team.
Power & Energy · data manager — Application Case
Project Background
The project covers boiler feedwater, turbine condensate and FGD/DeNOx systems. The work centres on data manager and the core task is centralised data acquisition, storage and forwarding to management platforms.
Operating Challenges
The medium and duty are characterised by high temperature and pressure with both steam and saline water, and drift under high temperature and pressure, with very costly unplanned outages. So data manager cannot be specified generically — it calls for selected by channel count, storage depth and forwarding protocol.
Solution
The Ainstru engineering team worked through the system components range: supplying as a full cabinet and signal-chain configuration. The configuration involves selected by channel count, storage depth and forwarding protocol, with these requirements in view: compliance with power-industry codes and unit availability targets.
Results
Since start-up the system has run steadily; the practical result is automatic backfill after outages, greatly improving data completeness.
Related Products
 Endress+Hauser
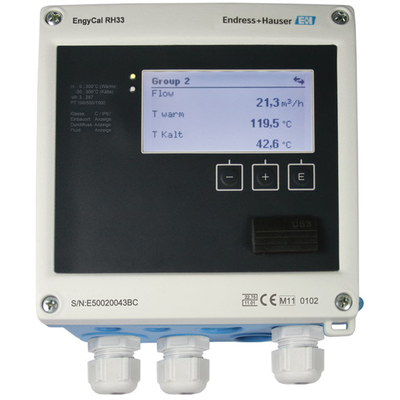
EngyCal RH33
 Endress+Hauser
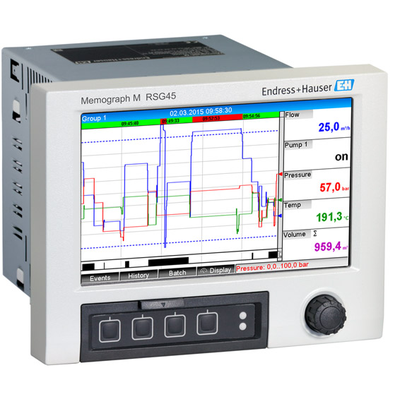
Advanced Graphic Data Manager RSG45
 Endress+Hauser
Energy Manager RMC621
 Endress+Hauser
Steam- and Heat computer RMS621
 Endress+Hauser
Ecograph T RSG35
 Endress+Hauser
Batch Controller RA33
 Endress+Hauser
Field Data Manager Software MS21
 Endress+Hauser