Technical Data
CompareProcess conditions
| Process pressure | -1 … +4 bar/-100 … +400 kPa (-14.5 … +58 psig) |
| Process temperature | -40 … +80 °C (-40 … +176 °F) Process temperature with mounting adapter -40 … +450 °C (-40 … +842 °F) |
| Ambient, storage and transport temperature | -40 … +80 °C (-40 … +176 °F) Hysteresis approx. 1.33 dB |
| Process connection | Thread from G1½, flange from DN 50 |
Electrical & communication
| Operating voltage | 20 … 55 V DC |
| Power consumption | max. 0.8 W Load current < 400 mA Voltage drop < 0.5 V |
| Switching voltage | < 55 V DC Reverse current < 10 μA |
Application area
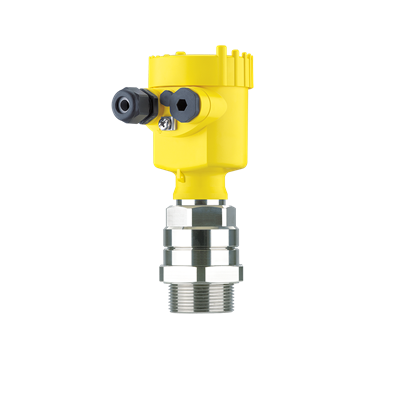
The VEGAMIP T61 is the emitting unit, the VEGAMIP R61 the receiving unit of the microwave barrier for level detection of bulk solids andliquids. Typical applications are the detection of bulk solids in silos,bunkers and crushers as well as of liquids in pipelines and vessels. Thenon-contact measuring principle has no direct contact with the mediumand ensures continuous wear-free and maintenance-free operation.
Your benefit
- Reliable measurement even with very abrasive products
- Simple adjustment saves time and costs with setup and commission
- ing
- Reliable measurement even with changing product properties
Function
The measuring system consists of a microwave emitter and a corresponding receiver. The emitted signal is focused by an antenna systemand radiated in the direction of the receiver. A medium in the path of thebeam damps the signal. This signal damping is detected by the receiverand converted into a switching signal. The built-in sensitivity adjustmentmakes it easy to adapt the instrument to the local conditions and themedium.
Case Studies
Municipal Wastewater Treatment · radar — Application Case
Project Overview
The site is the inlet, biological and outlet stages of a municipal plant. The customer wanted radar properly configured on the existing plant, with the aim of continuous radar level measurement of liquids and solids.
Technical Challenges
What actually causes trouble is high solids and corrosive fractions, with large diurnal flow swings, and effluent parameters drift and probes foul with sludge and biofilm. All of this means the radar configuration has to involve choosing antenna type by dielectric constant, range and process connection.
Configuration
Supply and installation were organised through the level range: level solution matched to the actual tank and silo geometry. On site this meant choosing antenna type by dielectric constant, range and process connection, checked line by line against: stable compliance with Grade 1A discharge limits and online data reporting.
Performance
After commissioning the outcome is reliable under heavy dust and vapour, reducing manual dipping, and the readings are now used for process tuning.
Food & Beverage · radar — Application Case
Site Conditions
This is a Food & Beverage customer whose plant is at dosing, pasteurising, filling and CIP stages. The main task was continuous radar level measurement of liquids and solids.
The Problem
The difficulty lies in syrups, dairy and beverages that scale easily, under strict hygienic requirements; at the same time frequent cleaning demands instruments that withstand hot CIP/SIP caustic cycles. Specification therefore means choosing antenna type by dielectric constant, range and process connection.
What We Did
We took a level range approach — level solution matched to the actual tank and silo geometry. Delivery was built around choosing antenna type by dielectric constant, range and process connection, with point-by-point checks on: food-safety and hygienic design per 3-A / EHEDG.
Operating Outcome
In service the system performs as intended — reliable under heavy dust and vapour, reducing manual dipping, with routine maintenance falling noticeably.
Chemical & Pharmaceutical · radar — Application Case
Application Context
reactors, metering vessels and finished-product tanks is a typical Chemical & Pharmaceutical duty. The project started from radar , focusing on continuous radar level measurement of liquids and solids.
Process Constraints
corrosion plus Ex protection shortens instrument life and makes downtime costly, and highly corrosive media with solvents and crystallisation, partly in explosive atmospheres only amplify it. The radar specification must therefore cover choosing antenna type by dielectric constant, range and process connection.
Delivery Approach
Delivery was handled as the level range — level solution matched to the actual tank and silo geometry. Execution centred on choosing antenna type by dielectric constant, range and process connection, together with Ex certification and GMP traceability of records.
Field Results
Operation shows the benefit clearly — reliable under heavy dust and vapour, reducing manual dipping, with confidence in this measuring point improving markedly.
Power & Energy · radar — Application Case
Customer Profile
The typical setting in Power & Energy is boiler feedwater, turbine condensate and FGD/DeNOx systems. The measuring point is radar ; the focus is continuous radar level measurement of liquids and solids.
Key Difficulties
Conditions are high temperature and pressure with both steam and saline water and, on top of that, drift under high temperature and pressure, with very costly unplanned outages, which a standard configuration cannot handle for long. The design therefore starts with choosing antenna type by dielectric constant, range and process connection.
Implementation
The scope ran through the level range: level solution matched to the actual tank and silo geometry. Technically it hinges on choosing antenna type by dielectric constant, range and process connection, and on these requirements: compliance with power-industry codes and unit availability targets.
Customer Benefit
In practice this means reliable under heavy dust and vapour, reducing manual dipping, which cut the workload on the site maintenance team.
Related Products
 Endress+Hauser
Micropilot FMR20
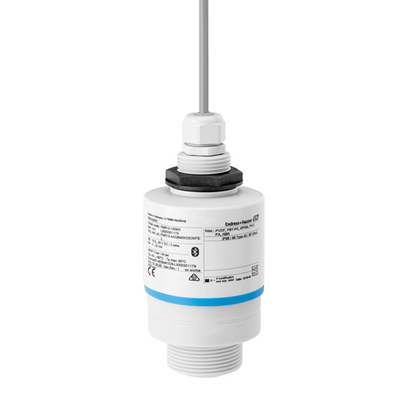 Endress+Hauser
Micropilot FMR10
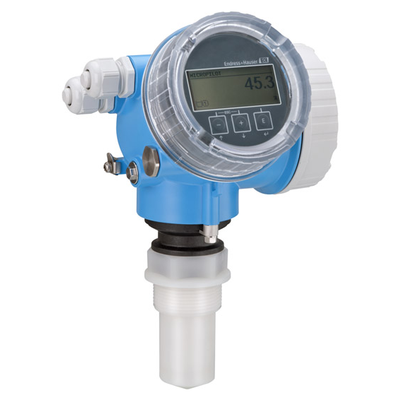 Endress+Hauser
Micropilot FMR50
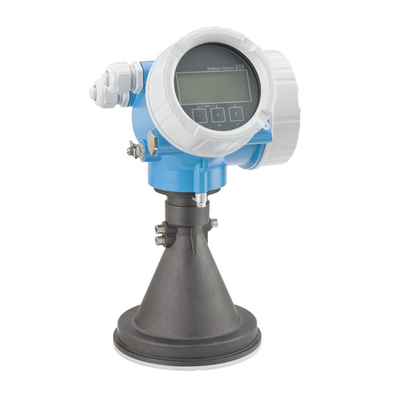 Endress+Hauser
Micropilot FMR56
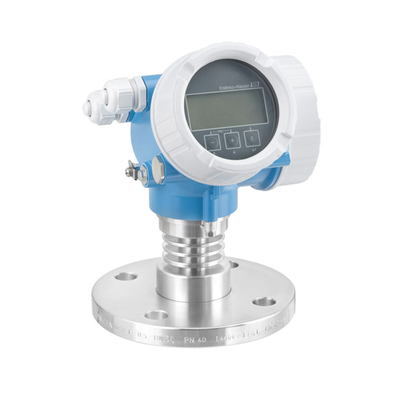 Endress+Hauser
Micropilot FMR52
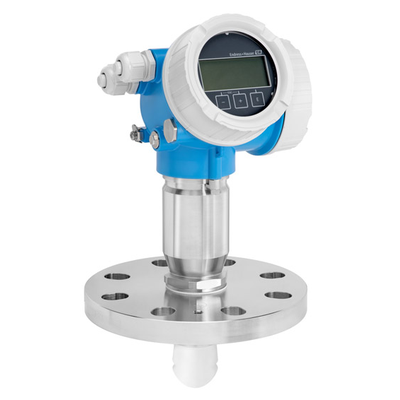 Endress+Hauser
Micropilot FMR60
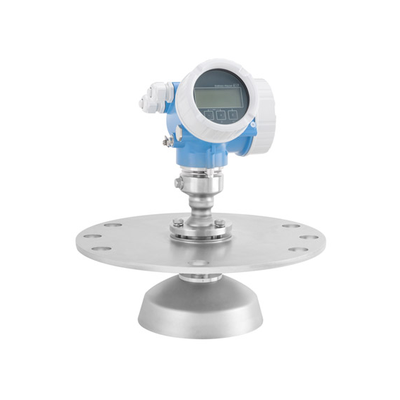 Endress+Hauser
Micropilot FMR57
 Endress+Hauser